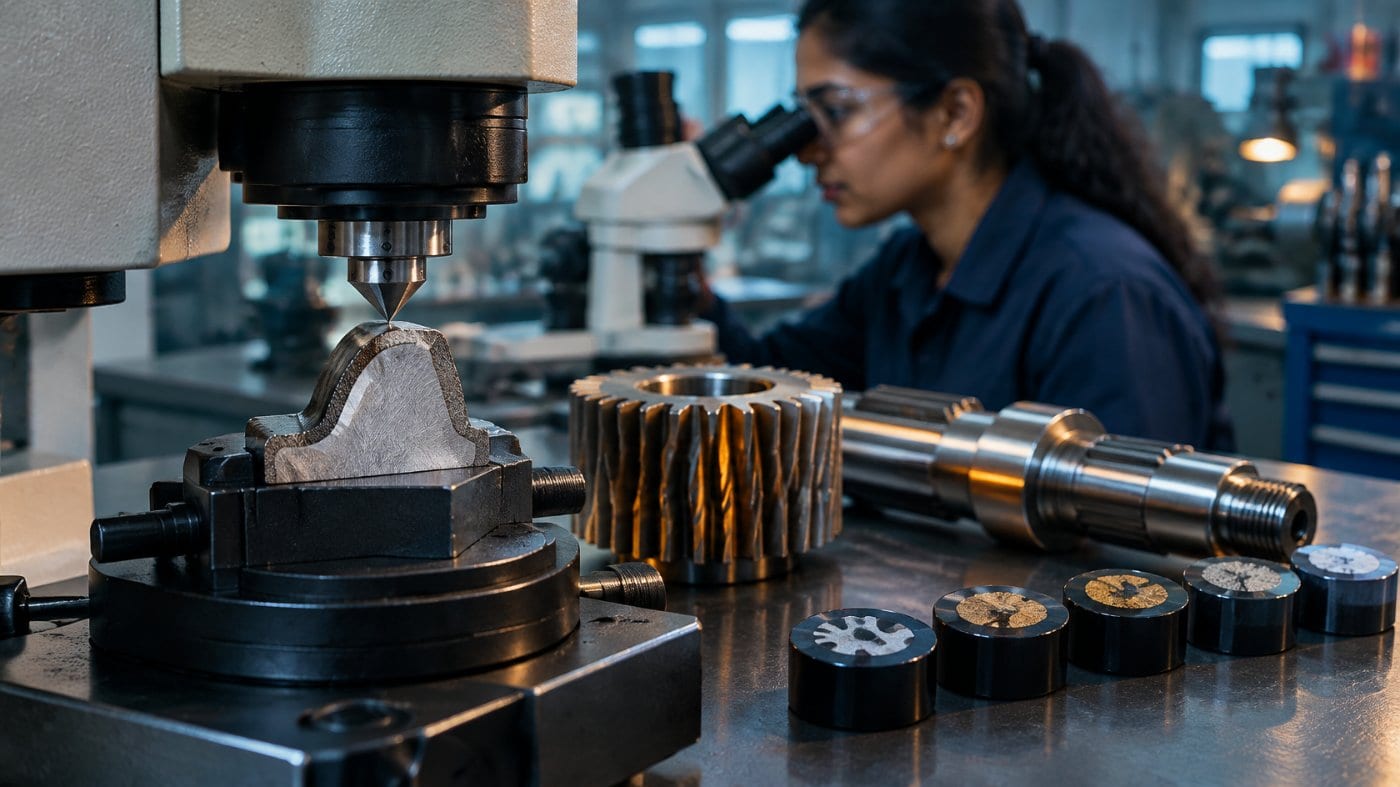
"Case harden and temper" is one of the most common notes on a shaft or gear drawing, and one of the most common causes of disputes between a machine shop, its heat treater and the customer. Without a hardness range, a case depth with its definition, and a clear note on where hardening is required, three people can read the same note three different ways. This guide explains what a complete heat treatment callout should contain and what to clarify before you quote.
Why vague heat treatment notes cause rejections
A heat treatment note controls properties you cannot see on the finished part. The machinist cannot measure case depth with a vernier. It needs a sectioned sample and a hardness traverse. So if the note is unclear, the problem usually shows up late: at the heat treater, at the customer's lab, or as a field failure.
Typical gaps found on drawings:
- "Case harden" with no depth or no hardness value.
- A case depth with no definition, so nobody knows whether it means effective or total depth.
- Surface hardness given as a single number, with no range.
- No indication of which surfaces must be hardened and which must stay soft, for example threads or areas machined after heat treatment.
- No test method, so the customer's lab and your heat treater measure differently.
Effective case depth vs total case depth
This is the point most often misread. An article in Thermal Processing explains that total case depth is the distance from the surface to where the case and core can no longer be told apart, while effective case depth is usually specified as the depth to a specific hardness. The article calls effective case depth "the most ambiguous" of the case depth terms and notes it is typically about 66 to 75 percent of the total case depth.
That gap matters. If the drawing says "case depth 0.8 mm" and your heat treater targets total depth while the customer checks effective depth, the part can fail inspection even though everyone did their job.
The 550 HV reference in ISO 2639
For carburised and hardened steels, ISO 2639 defines the case-hardened depth (CHD) as the perpendicular distance between the surface and the layer with a hardness of 550 HV 1. The standard also allows a higher limiting hardness, in steps of 25 units, for steels whose core is hard enough.
So a callout that names CHD and the standard removes most of the guesswork. The Thermal Processing article adds that the SAE approach and ISO 18203 define effective depth differently, which is one more reason to state the method on the drawing rather than assume it.
What a complete callout should contain
ISO 15787 is the international standard for presenting and indicating heat treatment of ferrous parts in technical documentation. Whatever format your customer uses, a usable note normally covers:
- Process: carburise, harden and temper; induction harden; nitride; through harden.
- Surface hardness as a range, with the scale, for example HRC or HV.
- Case depth with its definition, for example CHD at 550 HV 1, as a min-max range.
- Core hardness, where strength of the core matters.
- Zones: which surfaces are hardened, and which are kept soft or masked.
- Sequence: which dimensions are finished after heat treatment, such as grinding allowance.
Illustrative example: "Carburise, harden and temper. Surface 58-62 HRC. CHD 0.6-0.9 mm at 550 HV 1 per ISO 2639. Threads and keyway soft. Grind bearing journals after heat treatment." Every value here is an example, not a recommendation for your part.
If the drawing does not tell your heat treater and the customer's lab the same thing, the part is not first time right, however well it was machined.
What to clarify before you quote
Heat treatment affects cost in ways that are easy to miss: grinding allowance, straightening after distortion, masking for soft zones, cut-up samples for case depth checks, and lab test reports in the PPAP or inspection file. Before quoting, confirm:
- The material grade is suitable for the process, for example a carburising grade for carburising.
- The case depth definition and test method match what your heat treater can certify.
- How many test samples per batch the customer expects, and whether a sacrificial part is needed.
- Whether post-heat-treatment machining is yours or the customer's.
Put the assumptions you make in writing with the quote. It is far easier to agree a hardness range at RFQ stage than after a lot is on hold.
How SpecReview helps
SpecReview reads a drawing PDF and flags unclear notes such as incomplete heat treatment callouts as spec gaps to clarify before quoting, each tagged as from the spec, the geometry or an assumption. Its quality plan and layout inspection plan help you list hardness and case depth checks alongside the dimensional ones.